In brief

Show how the line presents the required features and associates each closure, code and visible-check result with the same vial or carrier. Define the active-job result set and the response to missing or uncertain results before final disposition. Agree those responsibilities in the interface review.

Plan vial closure code and visible checks around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems.

On the production floor

Plan for the conditions your team handles every day — Vial Closure Code and Visible Checks

Plan vial closure code and visible checks around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. For in-line inspection using vial closure, code and visible checks, the deciding details include visible defect or measurement definition for vial closure, code & visible checks, part presentation and production speed and false-accept, false-reject and challenge criteria.

Discuss your application
Your application

Details worth resolving early for in-line inspection using vial closure, code and visible checks

Question 1

Visible Defect or Measurement Definition for Vial Closure, Code & Visible Checks

For in-line inspection using vial closure, code and visible checks, describe the current position, required outcome, acceptable limits and known exceptions for visible defect or measurement definition for vial closure, code & visible checks. That lets us compare options against your real production rather than one nominal value.

Question 2

Good, Bad and Marginal Sample Range

For in-line inspection using vial closure, code and visible checks, describe the current position, required outcome, acceptable limits and known exceptions for good, bad and marginal sample range. That lets us compare options against your real production rather than one nominal value.

Question 3

Part Presentation and Production Speed

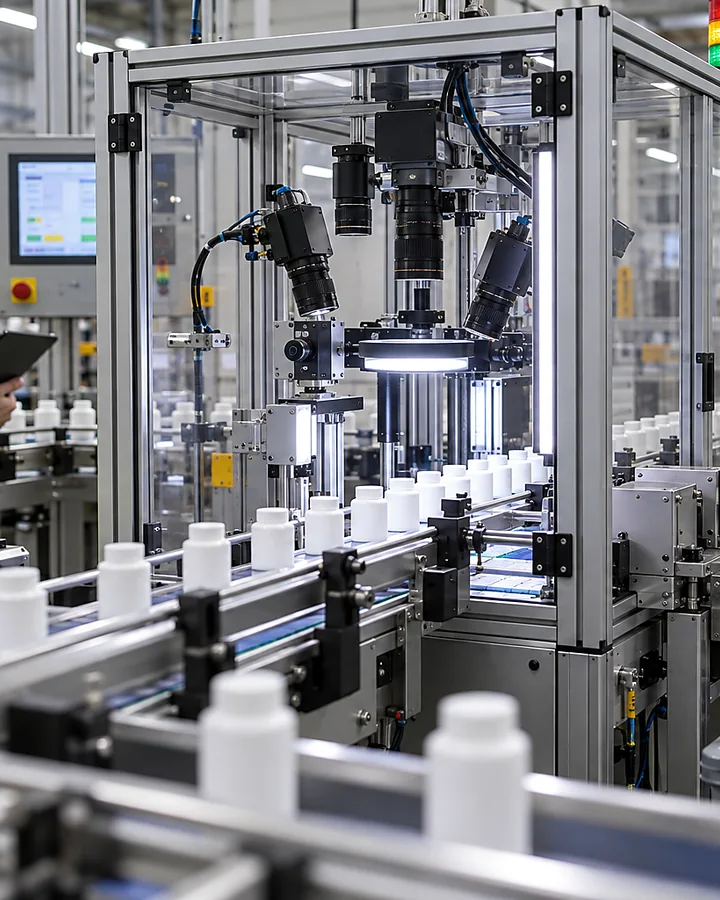
Record the vial-format range, spacing, expected rotation and transfer conditions at each view. Demonstrate that the required feature is observable under the intended presentation, and retain the limits of the tested coverage.

Question 4

Optics, Lighting and Environmental Conditions

For in-line inspection using vial closure, code and visible checks, describe the current position, required outcome, acceptable limits and known exceptions for optics, lighting and environmental conditions. That lets us compare options against your real production rather than one nominal value.

Question 5

Recipe, Reject and Line-Control Interfaces

For in-line inspection using vial closure, code and visible checks, describe the current position, required outcome, acceptable limits and known exceptions for recipe, reject and line-control interfaces. That lets us compare options against your real production rather than one nominal value.

Question 6

False-Accept, False-Reject and Challenge Criteria

For in-line inspection using vial closure, code and visible checks, describe the current position, required outcome, acceptable limits and known exceptions for false-accept, false-reject and challenge criteria. That lets us compare options against your real production rather than one nominal value.

Your operating cycle

Plan for more than automatic running

Include replenishment, normal production, planned change, short stops, fault recovery, cleaning and maintenance for in-line inspection using vial closure, code and visible checks. A fast automatic step can still leave your team with a slow or awkward overall process.

Prove the result

Test in-line inspection using vial closure, code and visible checks against representative good, bad and marginal samples

Normal production

Run the agreed product or part mix for in-line inspection using vial closure, code and visible checks at your intended operating pattern.

Difficult conditions

Include credible extremes for visible defect or measurement definition for vial closure, code & visible checks and good, bad and marginal sample range.

Fault and recovery

Challenge the agreed sequence with identified samples, an absent vial, changed spacing and a stop with vials between inspection and removal. Confirm how incomplete result sets are handled on restart and how a late result is kept from being assigned to the next vial.

Important limits

Be clear about what the trial has shown

Compare with Retrofit or Multi-Variant Checks Involving Vial Closure, Code and Visible Checks if that operating pattern is closer to your application.