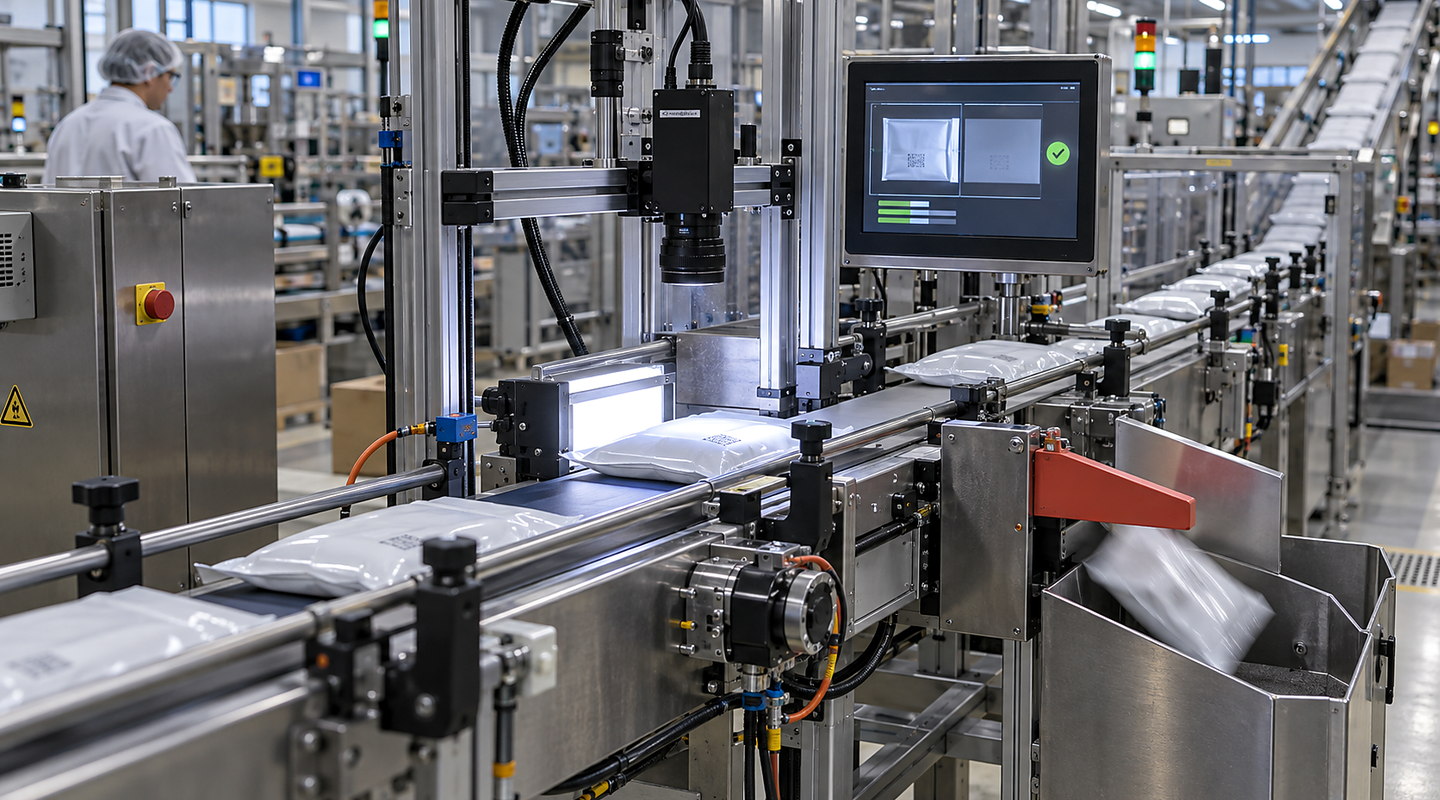
Vial Closure Code and Visible Checks Selection Guide
Choose vial closure code and visible checks by comparing your parts, process, rate, access, data needs and required results.
Compare proposals by demonstrated viewing coverage, approved sample diversity, correct job-data comparison and result-to-vial tracking. Require clear handling of missing or uncertain results and explicit limits for separate product requirements. Prepare the same inspection brief for each option.
For in-line inspection using vial closure, code and visible checks, a short trial that reproduces the difficult condition is often more useful than a long list of nominal specifications.
Compare options in the conditions where they must work — Vial Closure Code and Visible Checks
Plan vial closure code and visible checks around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. A useful shortlist should show how every option copes with visible defect or measurement definition for vial closure, code & visible checks and recipe, reject and line-control interfaces.
Discuss your application
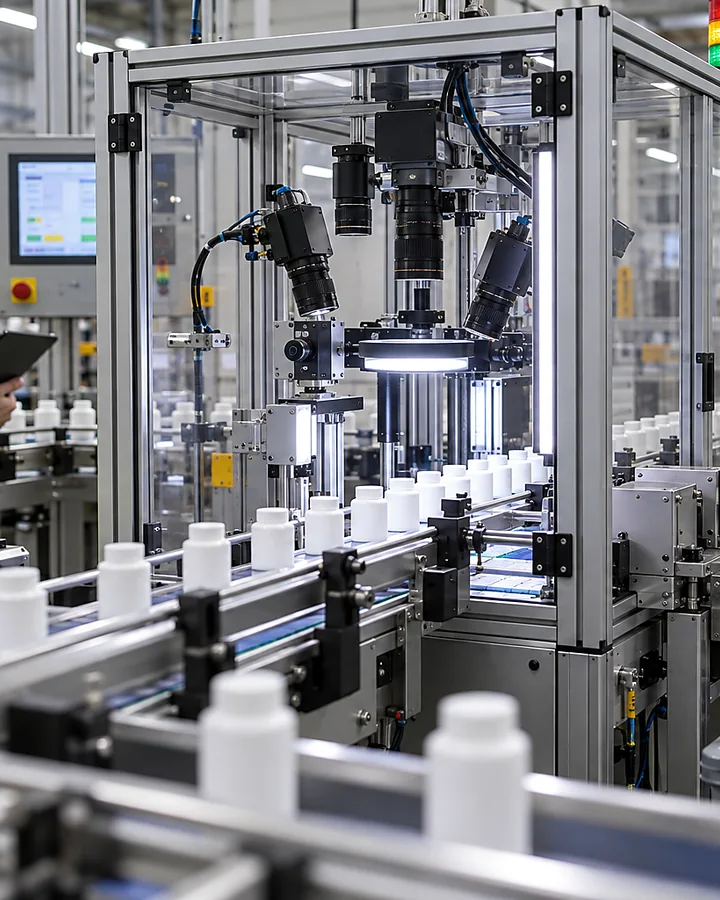
Ask every supplier the same questions
| Decision | What to ask | What to check |
|---|---|---|
| Visible Defect or Measurement Definition for Vial Closure, Code & Visible Checks | Which visible feature or printed field is assessed, and what decision is required from each view? | Approved sample decisions, required views and exclusions from optical coverage. |
| Good, Bad and Marginal Sample Range | Which labelled good, defective and marginal examples cover the actual vial, closure and print variation? | Responsible-quality-team expected results and the limits of the demonstrated sample range. |
| Part Presentation and Production Speed | How are format, spacing, rotation and transfer variation represented at each inspection view? | Recorded presentation trials showing that each required feature enters the view, with uncovered conditions identified. |
| Optics, Lighting and Environmental Conditions | Which viewing and lighting arrangement makes the required feature observable under the intended conditions? | Images or observations tied to the actual sample, format and setup; no inference beyond the tested view. |
| Recipe, Reject and Line-Control Interfaces | Who controls authorised job data and recipe versions, and how do complete results stay attached to the right vial? | Combined-sequence evidence for missing results, interrupted transfers, removal confirmation and restart reconciliation. |
| False-Accept, False-Reject and Challenge Criteria | How are missed defects, rejected good samples and uncertain results recorded and reviewed separately? | Agreed challenge results, observed disposition and ownership of unresolved cases; separate manufacturer release requirements. |
Include simpler approaches to vial closure, code and visible checks in your shortlist
| Approach | Often suitable when | Watch for |
|---|---|---|
| Vial Closure Code and Visible Checks | You need a dedicated solution for a clearly defined duty, product or part range and line interface. | Regulated-product validation and release decisions remain with the responsible manufacturer. |
| Purpose-Built Sensors for Simple Presence or Position Checks | The required decision is a simple presence or position check. | Use approved challenge samples and confirm that the required feature is visible under the intended presentation. |
| Offline Metrology or Destructive Tests where the Property Is Not Visible Inline | The required property is outside the demonstrated visual check. | Record the separate validated method and keep validation and release decisions with the responsible manufacturer. |
Pause before choosing when…
- Only perfect or hand-selected examples of in-line inspection using vial closure, code and visible checks are available.
- No one has defined how false-accept, false-reject and challenge criteria will be evaluated.
- The normal range for visible defect or measurement definition for vial closure, code & visible checks is described only as “usually fine” but has not been bounded.
- Your operator, cleaning, maintenance or recovery access has not been considered.
- Quoted performance depends on another machine or data source that is not included.